

Every machine is a row on the board. A machine can be a real machine, a bench, a department desk or an outside vendor. Machines are set up on Schedule › Setup › Machines & hours; only team admins can change them.
Import from Equipment#
The presses, printers, guillotines, cutting tables and platemakers you set up in Equipment can be added in one go: Add all to the schedule on the banner at the top of Machines & hours (or Choose which to pick some). Each becomes a machine linked to its equipment. A linked machine reads its size, speed and makeready from Equipment every time a job is timed, so you never keep two copies of the same numbers.
A flexo press becomes a Flexo press machine that runs at its web speed after its makeready, and a screen press a Screen press machine that runs at its prints per hour after its setup; a step on them is timed from that setup and rate.
A machine you archive in Equipment is switched off in the Schedule too. Steps that haven't started on it need another machine.
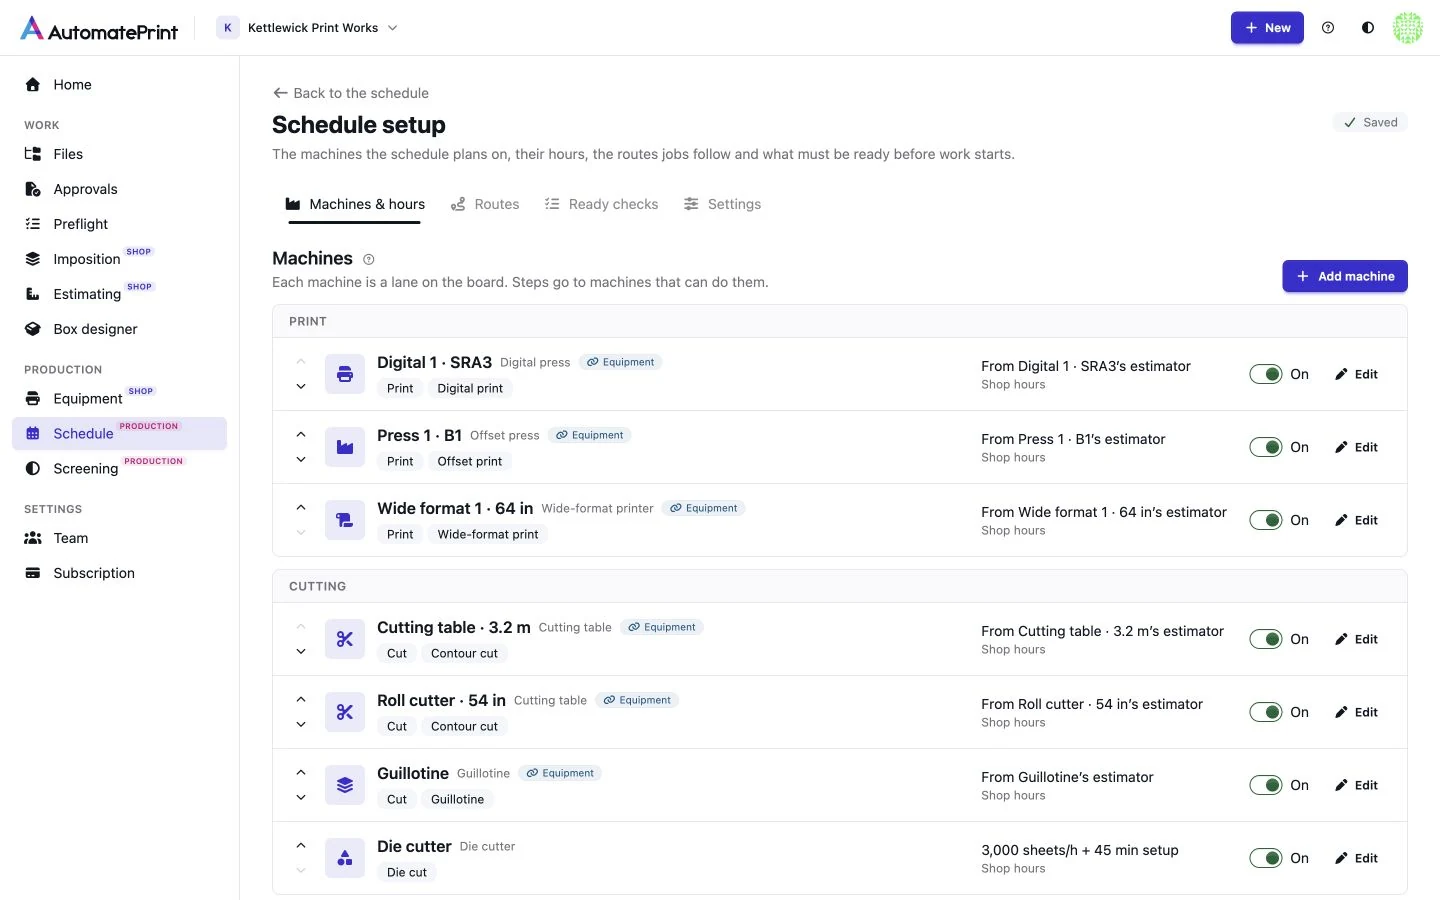
Add a machine#
Add machine adds a finishing machine, a bench or an outside vendor in about ten seconds.
The steps:
- Choose the kind (the tiles below; Custom is last).
- Give it a name, such as "Die cutter 1".
- Check the department. It is filled in from the kind and groups the rows on the board.
- Set its Setup and Speed, such as 15 min + 3,000 sheets/h. An outside vendor has a Usual turnaround instead.
More opens What it can do (its capabilities), its Hours, Wait before the next step (drying or curing time after this machine), Shortest run, Changeover between different jobs and notes. The new machine is a row on the board at once, and every step that needs one of its capabilities can go on it. The arrows on a machine's row change its place in its department.
| Kind | Department | Can do | Use it for |
|---|---|---|---|
| Platesetter | Prepress | Plates | Makes the plates of offset jobs. Linked to a platemaker in Equipment, it is timed by that platemaker for the press the job prints on; otherwise per plate at its own speed. |
| Offset press | Print, Offset print | A sheetfed offset press. Linked to a press in Equipment, it is timed by that press. | |
| Digital press | Print, Digital print | A digital press. Linked to a press in Equipment, it is timed by that press. | |
| Flexo press | Print, Flexo print | A flexo press printing a roll. Linked to a flexo press in Equipment, it runs at that press's web speed after its makeready. | |
| Screen press | Print, Screen print | A screen press: a garment carousel, a flatbed or a cylinder press. Linked to a screen press in Equipment, it runs at that press's prints per hour after its setup. | |
| Wide-format printer | Print, Wide-format print | A wide-format or roll printer. Linked to a printer in Equipment, it is timed in the job's mode. | |
| Cutting table | Cutting | Cut, Contour cut | A digital cutting table. Linked to a cutter in Equipment, it is timed from the solution's cuts. |
| Guillotine | Cutting | Cut, Guillotine | A guillotine. Linked to one in Equipment, it is timed from the solution's knife program. |
| Die cutter | Cutting | Die cut | A platen or rotary die cutter, timed from its setup and speed. |
| Folder | Finishing | Fold | Folds flyers and signatures. |
| Folder-gluer | Finishing | Fold, Glue | Folds and glues carton blanks. |
| Laminator | Finishing | Laminate | Laminates sheets or roll prints. |
| Binder | Finishing | Bind | Perfect binding, wire binding and other binding. |
| Stitcher | Finishing | Bind, Stitch | Saddle stitching. |
| Mounting | Finishing | Mount | Mounts prints on board or panels. |
| Packing | Finishing | Pack | Counts, wraps and boxes finished work. |
| Shipping | Shipping | Ship | Dispatch: the last step before a job leaves. |
| Outside vendor | Outside | Outside vendor | Work another company does. It has no queue: each step takes the vendor's lead time. |
| Custom | Finishing | What you name | Anything else, such as grommets or hand finishing. You name what it can do. |
Capabilities#
A step asks for a capability, such as Fold, and can go on any active machine that has it. Each kind of machine starts with its own. You can add your own tags too, such as "UV", "Coater" or "Food-safe", and a route step can require one ("Must have: Coater"). A custom machine has only the capabilities you give it: name a new one, such as "Grommets", and routes can ask for it.
| Capability | Machines that have it | A step that needs it |
|---|---|---|
| Plates | Platesetter | Making the plates of an offset job. |
| Offset press, Digital press, Flexo press, Screen press, Wide-format printer | Any printing step. | |
| Offset print | Offset press | Printing on an offset press. |
| Digital print | Digital press | Printing on a digital press. |
| Wide-format print | Wide-format printer | Printing on a wide-format printer. |
| Flexo print | Flexo press | Printing on a flexo press (narrow-web labels, or a flexo folder-gluer for boxes). |
| Screen print | Screen press | Printing on a screen press (garments, posters, signs, panels). |
| Cut | Cutting table, Guillotine | Any cutting step. |
| Contour cut | Cutting table | Cutting along shapes. |
| Guillotine | Guillotine | Straight cuts on a guillotine. |
| Die cut | Die cutter | Cutting with a die. |
| Fold | Folder, Folder-gluer | Folding. |
| Glue | Folder-gluer | Gluing. |
| Laminate | Laminator | Laminating. |
| Bind | Binder, Stitcher | Binding. |
| Stitch | Stitcher | Stitching. |
| Mount | Mounting | Mounting. |
| Slit and rewind | Machines you tag | Slitting a printed roll into narrower rolls and rewinding them, as label work needs. |
| Pack | Packing | Packing. |
| Ship | Shipping | Shipping. |
| Outside vendor | Outside vendor | A step an outside vendor does. |
Where step times come from#
| Machine | How its steps are timed |
|---|---|
| Linked offset or digital press | The press's own estimate for the imposed sheets: makeready for the plates and passes, then the run and any wash-ups. |
| Linked printer | The printer's estimate in the job's print mode, including handling. Its drying time is a wait before the next step. |
| Linked guillotine | The solution's knife program: setup, jogging and cutting for every lift. |
| Linked cutting table | The solution's cut paths on that table, with its setup and registration. |
| Linked platemaker | The platemaker's estimate for the job's plates on the press the job prints on: setup, imaging and handling, with its remake allowance. Its process wait holds the press until it has passed. |
| Platesetter not linked to Equipment | Its setup time plus the job's plates at its rate. The plates are those of the solution's ink plan (a 4/4 form printed sheetwise needs 8), or else CMYK per side from the press's estimate. |
| Any other machine | Its setup time plus the quantity at its rate, never less than its minimum run time. |
| Outside vendor | Its usual turnaround, in hours on the clock (a vendor has no hours of its own). |
The times are the same ones the imposition report shows for the machine the solution was planned for. They are worked out when the job arrives, and again when the solution or the equipment changes, never while you look at the board.
Approximate times#
A step shows ≈ when its time is an approximation:
- the step is on another press than the one the job was imposed for (the plates and passes were planned for that press; open the job in Imposition to re-impose it for this one);
- the printer doesn't have the job's print mode, so its own default mode is used;
- the guillotine only has the slitting of a strips solution, not a full knife program;
- the job's plate count isn't known (no ink plan and no press estimate), so a platesetter not linked to Equipment only gets its setup time;
- the machine's estimate couldn't be worked out (for example, the solution has no knife program yet), so the machine's setup time and rate are used. Hover the ≈ to see why.
Plates are made for one press#
A job's plates are made for the press that prints it: their size, and whether the platemaker can take it, come from that press. Move the print step to another press before the plates are made, and the Plates step is timed again for that press. Once the plates are done, a move to a press that takes another plate size isn't re-timed: the print step gets the conflict The plates were made for a press with another plate size and planners get a Plates must be remade alert. Move printing back, or make the plates again.
Makeready between jobs#
Makeready grows when the next job needs a change. Set the minutes for each kind of change under Changeover between different jobs: Spot ink wash (per ink), Stock change, Sheet size change, Coating change, Plate change, Die change and Knife program change. Process and house inks never count as a change. Plate change counts when the next job is on another plate or sleeve set: a repeat job on the same plates skips it (put the plate change time here rather than in the setup time, so a repeat saves it). On a linked press, the spot-ink wash-up is the press's own. Because this is worked out from each job's neighbour on the machine, changing the order changes the makeready. The first step in a machine's queue is compared with the last job the machine finished; when that isn't known, only the setup time counts.
Placing and Re-plan use these minutes to batch: jobs that share spot inks, plates, stock or a die run back to back when that doesn't make a job late, so the press washes up or changes over less. A job's inks, plates and stock come from its imposition, or, for a job added by hand, from Inks, plates and stock (see Adding and editing jobs).
Outside vendors#
An Outside vendor machine is for work another company does: foiling, special binding, mounting. It has no queue: every step sent to it starts when it is ready and takes the vendor's lead time, however many other jobs are there. It has no hours of its own, so the turnaround counts every hour, nights and weekends too: enter 48 for two days. Its steps still count toward the job's finish date.
Planned: Later
Duration overrides per step, and suggestions to correct a machine's speed from its actual times (for example "Runs 18 % slower than estimated. Apply ×1.18"), are planned. A suggestion is never applied without you.