

An offset run prints each form a run length. The run chooses which items go on which form, how many copies of each item a form holds (its slots), and how many sheets each form runs, so every item gets close to its ordered quantity at the lowest cost.
Forms and plates#
A form is one sheet layout, front and back, printed as one run of good sheets. Each form needs its own plate set: one plate for every ink on every printed side. So a plan of 2 forms printed 4/4 (CMYK on both sides) uses 16 plates, 8 per form (4 + 4). Where one form is shown, its plates are shown by side, such as "8 (4 + 4)".
Plates are counted for every offset form, with or without a press and with or without known inks:
- Process inks count one plate each, spot colours one more each.
- A flood coating on a coater of the press needs no plate; printed from an ink unit it counts one. Without a press, a flood coating counts one plate ("Counted without a press").
- A spot varnish counts one plate when the press prints it inline; cold foil counts one (its adhesive); hot foil, embossing and debossing are tooling, not plates.
- An item whose inks aren't known counts as CMYK on each side it prints: 4 plates single-sided, 8 two-sided. The count is marked assumed 4/0, assumed 4/4, or assumed when the form mixes both.
- A digital press uses no plates: the Plates column shows "—".
- Work-and-turn and work-and-tumble are counted sheetwise for now (8 plates for a 4/4 form), because every form is imposed sheetwise.
The item inks come from the artwork's files or are set by hand (see Item inks: detected and declared). Plates are counted when the run plans; the solution on screen, the Report, the Production tab and the exports count again from the current item inks, so editing an item's inks shows at once.
The Press run card#
The Press run card sets what an offset plan works within: the most forms, the overrun and underrun caps, makeready, spoilage and costs. It shows on the Production tab when Offset is chosen in the run bar.
| Setting | API field | Default | Range | What it does |
|---|---|---|---|---|
| Max forms | max_plates | Empty | 1 to 99 | The most forms the plan may use (a form is one sheet layout, front and back, with its own plate set), up to 99. Every form count up to this is planned and compared. Empty (Auto): every count up to one form per item, and the cheapest wins. |
| Overrun % | overrun_pct | 10 | 0 to 500 | How far above its ordered quantity an item may be produced. Empty: any. |
| Underrun % | underrun_pct | 0 | 0 to 50 | How far below its ordered quantity an item may be produced. |
| Makeready sheets | makeready_sheets | 250 | 0 to 10,000 | Sheets spent setting up each form before good sheets. |
| Spoilage % | spoilage_pct | 0 | 0 to 50 | Extra sheets printed on top of the run and makeready, for waste. |
| Extra cost per form | form_extra_cost | Empty | 0 or more, or empty | Money added once per form on top of the plates (proofs, a share of a die). Empty: none. |
| Plate set cost (per form) | plate_set_cost | Empty | 0 or more, or empty | The cost of one form's plate set, used only when no platemaker and no press plate cost prices the plates; otherwise the card shows it as ignored. Empty: none. |
| Sheet cost (per sheet) | sheet_cost | Empty | 0 or more, or empty | The cost of one printed sheet. Empty: every sheet costs 1, so the plan with the fewest printed sheets wins. |
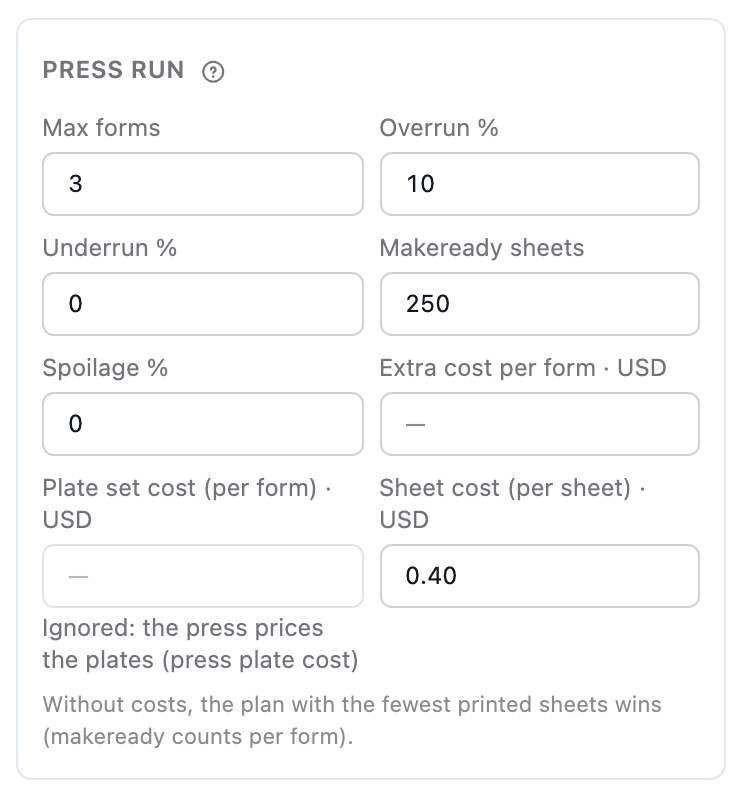
Lengths don't apply: every value is a count, a percentage or a cost. The same fields are on the job in the API (see
Imposition API); Max forms keeps its API name, max_plates.
Each item can also have its own Over % and Under % in the item list (Item properties); an item without them uses these values.
Max forms is empty (Auto) on a new job: every form count from 1 up to one form per item is planned and the cheapest plan wins, so you don't have to guess how many forms the job needs. Type a number, up to 99, to cap it: no plan then uses more forms than that. Planning on a die works the same way (Standing dies).
How a plan is counted#
For each form, the sheets printed are the run plus the makeready, plus spoilage on both:
printed = (run + makeready sheets) × (1 + spoilage %), rounded up
For example, a form with a run of 1,000, 250 makeready sheets and 2 % spoilage prints 1,275 sheets.
Each item's pieces are its slots on every form × that form's run. They must fall between:
- at least the ordered quantity less the Underrun % (0 % by default: never fewer than ordered), and
- at most the ordered quantity plus the Overrun % (10 % by default; empty allows any overrun).
So an item of 1,000 with the defaults may be produced 1,000 to 1,100 times.
How plates are costed#
A job's plates are priced from exactly one place, in this order:
- A platemaker of the team (Equipment, Platemaking tab) that takes the press's plate: its plate material, time and rates. The solution then gets a Plates step before printing.
- The press's plate cost per plate. A plate cost of 0 means the press's rate includes plates: the plates read "included in press rate".
- The job's Plate set cost (per form) × forms, when neither of the above prices plates.
- Otherwise the plates read Plates not priced, never $0.
Extra cost per form always counts: it is money added once per form on top of the plates, such as proofs or a share of a die. Plate set cost (per form) counts only in case 3; when a platemaker or the press prices the plates the card shows it as ignored ("Ignored: plates are costed by Platesetter A", "Ignored: the press prices the plates") and the Production tab notes that the job's plate set cost is ignored. A job saved with the earlier single plate cost field kept its value in the field it meant: the extra cost when the job's press had a plate cost, else the plate set cost.
The plates are their own row on the Production tab and their own Plates $ column on the Compare tab. The press's minimum charge still covers the press and its bought plates together, so a press with a minimum prices the same as before.
How plans are compared#
A plan is made for every form count from 1 to Max forms (with Auto, up to one form per item). Each one is checked: every item within its caps, the totals right, and every form a valid layout. Each plan is a row on the Compare tab, so you can compare, say, 2 forms against 3.
With an ink model on the press (a press and known item inks), a plan's cost is its printed sheets × Sheet cost (per sheet) plus every plate and pass at the press's rates, plus the extra cost per form. Without one, the planner estimates each form's plates as if it held every item's inks, and prices them per form with the plate source's per-plate money; this approximation only ranks plans, and the Report prices the plates each form really uses. Without costs every sheet counts 1 and plates are free, so the plan with the fewest printed sheets wins; makeready still counts for every form. Set the costs when plates are expensive compared with paper.
More time can find a better plan, especially when the job has many items.
Reading the result#
The Production tab's Forms & impressions table lists each form: the artworks and their slots, its plates by side, the run, the makeready and the sheets printed, with the plan's total ("2 forms · 16 plates · 2,185 printed sheets") and its Plates row. Overrun per artwork shows each item's ordered and produced pieces and its overrun: red when it is outside the caps, amber within one point of the overrun cap.
The export menu adds a Run sheet (CSV), a Plate list (CSV) and one PDF per form, Form 1 PDF, Form 2 PDF and so on (see Exports).
When there is no plan#
If no plan meets the caps, the run finishes with a note instead of solutions, such as "No plan within 10 % overrun on 3 forms; try 4 forms or allow more overrun." Raise Max forms, allow more overrun or some underrun, or give the run more time. An artwork that doesn't fit the sheet at any allowed angle is named in the note. See Troubleshooting runs.
Warning: Press times are estimates from your wide-format equipment
The Production tab times and prices offset and N-up sheet work with the team's printer and cutter. Until sheetfed presses and guillotines can be set up as equipment, those times come from your wide-format printer and flatbed cutter, and may not match a sheetfed press or a guillotine.